Buying a Cnc Die Welding Machine is not simply a matter of comparing prices. The decision affects die life, repair accuracy, operator safety, and production downtime. Recent reports from Grand View Research and MarketsandMarkets show continued growth in CNC machinery and welding-equipment demand, driven by automation, tighter tolerances, and labor shortages. Those trends matter on the workshop floor. A machine may promise high power, yet still produce uneven beads around a sharp die corner.
Dr. John C. Lippold, a recognized welding-metallurgy expert, has often stressed that “welding is fundamentally a metallurgy problem, not just a heat problem.” This principle should guide every purchase. Buyers need to examine pulse control, wire-feeding stability, laser or arc compatibility, cooling performance, fixture access, and software repeatability. The best Cnc Die Welding Machine should match the die material, repair thickness, and daily workload. Ask for test welds on your own steel. Watch the heat-affected zone closely.
Small details matter.
ISO 3834 and AWS guidance also highlight qualified procedures, traceability, and consistent inspection. A machine without reliable records may create expensive uncertainty later. Supplier support deserves equal attention. Check training, spare-part availability, calibration service, and response times. A low purchase price can become costly after one failed repair.
No checklist is perfect. I would still leave room for doubt. Marketing claims rarely show awkward corners, contaminated surfaces, or tired operators at midnight. This guide’s ten tips focus on those practical gaps, helping buyers compare equipment with evidence rather than excitement.
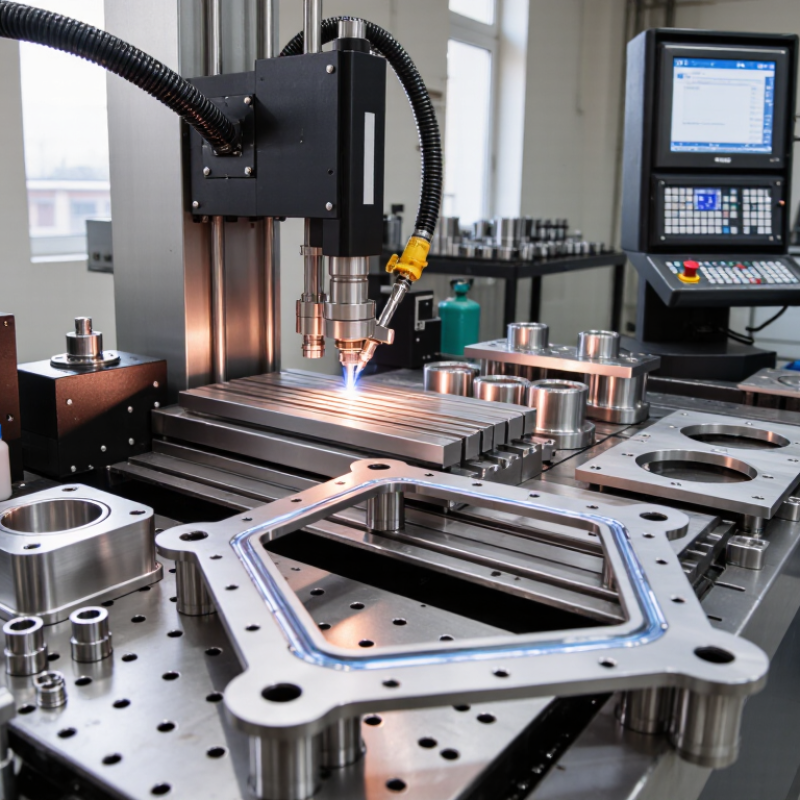
A practical buying decision starts with a clear welding requirement. Identify the die materials, dimensions, alloy types, and typical damage patterns. Small cracks need different control than deep cavities or broken edges. Measure the repair area carefully. Measure it twice.
Record the required welding current, wire diameter, heat input, and working temperature. These details affect penetration, distortion, and the heat-affected zone. Ask whether the machine supports your tolerances, especially around parting lines and sharp corners. An experienced technician can also assess operator access and fixture limitations. Numbers expose gaps.
Your production goal should be equally specific. Estimate repairs per shift, average welding time, setup time, and acceptable rework rates. If the machine will support continuous production, examine duty cycle, cooling performance, maintenance access, and process records. A repair shop may value flexibility, while a toolroom may prioritize repeatable results. Our first production estimate was wrong because cleaning and inspection took longer than welding. That mistake changed our capacity calculation. Include training time, spare consumables, and inspection steps in the budget. A lower purchase price can become expensive when operators fight unstable settings or frequent downtime. Define success with measurable targets, such as fewer rejected dies, shorter repair cycles, and consistent bead appearance.
Before selecting a CNC die welding machine, compare the expected production rate with the required cycle time. The planning scenarios below show how higher output targets generally require shorter cycle times and stronger automation capability. Confirm these benchmarks with your actual die size, weld length, material thickness, operator availability, and quality requirements.
Buying a CNC die welding machine starts with comparing its welding method, not its advertised power. Laser die welders create small, controlled heat zones and suit thin edges, cavities, and precision repairs. Micro-TIG systems offer strong deposits on larger damaged areas, but they can create more heat distortion. Wire-feed models improve filling speed, although they may need extra machining afterward.
Check the laser power or welding current carefully. Higher output is not automatically better. Pulse energy, pulse frequency, spot diameter, and wire size show how precisely the machine can work. A 0.2 mm spot may protect a sharp cavity edge, while a wider spot can repair a broad worn surface faster. That trade-off matters. It is easy to overlook.
Review the CNC travel range, axis repeatability, table load, and work envelope. A machine may have excellent accuracy but still reject a large die. Ask for test welds using your actual tool steel, cavity geometry, and filler wire. Inspect the heat-affected zone under magnification. Also check cooling capacity, fume extraction, software controls, and service access. Operators often lose time through awkward setup, not welding speed. A clear interface helps, but training remains essential. I would also question optimistic cycle-time claims, because cleaning, clamping, inspection, and finishing are rarely included.
10 Tips for Buying a CNC Die Welding Machine
Tip 1: Examine the control system before judging the machine’s speed. The screen should show welding paths, alarms, and parameter changes clearly. Tip 2: Check whether operators can save and recall proven programs. Tip 3: Ask for password levels and change histories. These features reduce accidental adjustments. Tip 4: Test the interface with gloves. A beautiful display is useless if commands feel confusing.
Tip 5: Study automation beyond marketing language. Automatic torch movement, fixture loading, and seam tracking should match your actual die workload. Tip 6: Confirm the machine’s accuracy through a sample weld. Measure torch position, bead placement, and repeatability at different travel speeds. Tip 7: Inspect calibration procedures. They should be practical, documented, and possible without unusual tools. A tiny alignment error can spread across a long repair seam.
Tip 8: Verify compatibility with your dies, welding materials, power supply, and existing fixtures. Tip 9: Request data on software communication and file formats before purchase. Closed systems may create future problems. Tip 10: Evaluate training, manuals, spare parts, and remote technical support. Reliable documentation often matters more than a faster cycle. A useful shop-floor lesson is simple: test real workpieces, not only demonstration blocks. I once overlooked fixture access during an evaluation. The machine met its accuracy claim, yet setup became inconvenient. Recheck clearance, operator visibility, and maintenance access before signing.
| No. | Buying Tip | What to Evaluate | Practical Benchmark or Requirement | How to Verify | Risk if Overlooked |
|---|---|---|---|---|---|
| 1 | Define the Die and Part Envelope | Maximum die length, width, height, weight, clamping area, and access for loading and unloading. | Select a working envelope that exceeds the largest planned die by at least 10–20% in each critical direction. Confirm table load capacity with a safety margin. | Submit representative drawings and a completed die-weight list to the supplier. Request a dimensional fit check. | Restricted travel, unsafe loading, or the need for manual rework. |
| 2 | Evaluate the CNC Control System | Axis control, program storage, user interface, alarm history, parameter access, password levels, and data backup. | Prefer a multi-axis CNC system with readable diagnostics, protected parameters, program backup through standard industrial interfaces, and clear recovery procedures. | Run a sample program, review alarm screens, test data backup, and confirm operator access levels. | Longer troubleshooting time, program loss, and inconsistent operation between shifts. |
| 3 | Check Positioning and Welding Accuracy | Axis repeatability, positioning accuracy, torch or electrode alignment, fixture repeatability, and thermal distortion control. | Use the supplier’s stated accuracy only as a starting point. Require documented acceptance results under the intended load and welding cycle; repeatability should be suitable for the tightest feature on the die. | Conduct a witnessed test using a representative fixture and measure critical locations with calibrated inspection equipment. | Misaligned welds, dimensional variation, increased grinding, and rejected parts. |
| 4 | Assess Automation Level | Automatic loading, fixture clamping, seam tracking, torch height control, wire feeding, parameter selection, and part changeover. | Automate repetitive operations that directly affect consistency, while retaining manual access for setup, inspection, and maintenance. | Calculate cycle time for setup, welding, inspection, and changeover using actual production scenarios. | Higher labor content, operator-dependent quality, and lower equipment utilization. |
| 5 | Confirm Welding Process Compatibility | Supported welding process, material grades, thickness range, joint geometry, shielding gas, filler wire, and heat input requirements. | The machine must support the required current, voltage, duty cycle, torch configuration, wire diameter, and gas flow range for every planned material and joint type. | Run weld trials on production-grade material and inspect appearance, penetration, distortion, and mechanical or non-destructive test results where applicable. | Poor penetration, excessive spatter, porosity, distortion, or inability to qualify the process. |
| 6 | Review Fixture and Workholding Compatibility | Fixture mounting pattern, clamping force, datum strategy, quick-change capability, grounding, and access for the welding torch. | Use repeatable datums and positive location features. Ensure clamps do not obstruct torch travel or create heat-related movement. | Inspect the proposed fixture design in a 3D simulation or physical trial. Verify grounding resistance and clamp accessibility. | Part movement, weld obstruction, long setup times, and inconsistent dimensions. |
| 7 | Measure Throughput and Cycle Time | Arc-on time, indexing time, loading and unloading, parameter changes, inspection time, and planned maintenance. | Compare total cycle time rather than welding speed alone. Include realistic pauses, consumable changes, fixture changes, and operator handling. | Request a timed demonstration with representative dies and record the complete end-to-end cycle. | Capacity shortfalls, missed delivery targets, and inaccurate return-on-investment calculations. |
| 8 | Verify Safety and Fume-Control Provisions | Guarding, interlocks, emergency stops, light curtains or door switches, electrical protection, grounding, and welding-fume extraction. | The installation should comply with applicable local machinery, electrical, welding, and occupational-safety requirements. Fume extraction must be sized for the process and enclosure. | Review the risk assessment, safety circuit documentation, extraction airflow data, and commissioning test records. | Operator exposure, unplanned shutdowns, regulatory non-compliance, and accident risk. |
| 9 | Check Integration and Data Compatibility | Electrical supply, compressed air, shielding gas, network connection, production software, barcode or recipe management, and quality records. | Confirm voltage, frequency, power demand, air pressure, gas requirements, communication protocols, file formats, and available network interfaces before purchase. | Use an integration checklist and test representative program files, recipe retrieval, data export, and system alarms. | Installation delays, manual data entry, incompatible files, and weak production traceability. |
| 10 | Evaluate Serviceability and Total Cost of Ownership | Preventive-maintenance intervals, spare parts, consumables, calibration, remote support, training, warranty, and energy consumption. | Compare total ownership cost over the planned service life, not only the purchase price. Require maintenance schedules, critical-spare recommendations, training scope, and response commitments in writing. | Request a five-year cost model and inspect the service documentation, training plan, and spare-parts availability. | Unexpected downtime, expensive consumables, slow repairs, and higher lifetime operating cost. |
Tip: Check the machine’s build quality before discussing price. Inspect the frame, welding head, rails, clamps, and cable connections closely. Solid components should move smoothly without unusual vibration or rough noise. Ask for sample welds on the same die material used in your workshop. Look for even bead formation, stable penetration, and minimal spatter. A polished demonstration is useful, but production testing matters more.
Tip: Review every safety feature with the operator present. Confirm emergency stops, protective guards, door interlocks, grounding, and temperature controls. The control panel should display faults clearly, not hide them behind technical codes. Ask how the machine handles overheating or interrupted power. Small safety details often prevent expensive downtime. I would also observe whether operators can reach controls without leaning across hot work areas.
Tip: Evaluate service and training before signing anything. Request installation guidance, maintenance schedules, troubleshooting instructions, and realistic response times. Training should cover setup, parameter changes, cleaning, inspection, and safe shutdown procedures. Ask who teaches the course and whether practical exercises are included. A manual alone is rarely enough. In my experience, rushed training creates avoidable mistakes during the first month. I have underestimated this before. Leave room for questions, because the machine may behave differently in your actual workshop. Ensure spare parts and technical support remain available after installation.
Buying a CNC die welding machine requires more than comparing purchase prices. Build a five-year total ownership cost model before requesting a final quotation. Include machine price, shipping, installation, operator training, tooling, electrodes, shielding gas, electricity, software, calibration, repairs, and planned downtime. Calculate cost per production hour, not only cost per unit.
McKinsey reports that predictive maintenance can reduce machine downtime by 30–50% and maintenance costs by 18–25%. Ask whether the supplier provides fault-history records, remote diagnostics, spare-parts availability, and a preventive maintenance schedule.
Energy use also matters. The U.S. Department of Energy states that compressed-air systems can lose 20–30% of input energy through leaks. If the welding cell needs compressed air, request measured consumption at your actual duty cycle.
Verify the supplier before signing. Check legal registration, factory ownership, export experience, quality procedures, and references from comparable metalworking operations. ISO’s 2023 Survey recorded more than 1.2 million ISO 9001 certificates worldwide, but certification alone proves limited practical capability. Request a current certificate and confirm its scope with the issuing body. Require a witnessed sample weld, dimensional inspection report, warranty terms, response times, and a parts list. A video tour is useful, but it is not an audit. One overlooked issue is installation support; an inexpensive machine may become costly when commissioning takes weeks. Leave room for doubt. Quotes often exclude cables, fixtures, software licenses, or operator travel.


All of Hapco's formulations are completely free of Mercury.
Hapco has been in business for over 50 years!
*NOTICE* Hapco will be will be closed on Monday, May 26th, in observance of Memorial Day. |
| Cookie | Duration | Description |
|---|---|---|
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytics". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Necessary". |
| cookielawinfo-checkbox-others | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Other. |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |